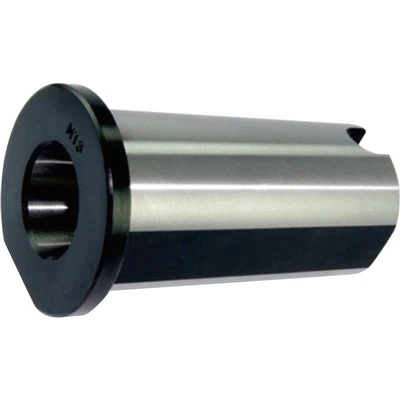
Product Introduction
At its core, the ER Collet Chuck is a specialized toolholding system consisting of a chuck body, interchangeable ER collets, and a clamping nut. The chuck interfaces with CNC milling machines, lathes, and machining centers, while the collets-available in a comprehensive range of sizes (from ER8 to ER50)-accommodate cylindrical tool shanks of varying diameters. Each component is manufactured to meet or exceed rigorous international standards, including DIN ISO 15488 and DIN 6499, ensuring consistent performance across applications.
The system operates on a simple yet highly effective principle: when the nut is tightened, the collet's tapered flexure sleeve compresses, creating uniform clamping pressure around the tool shank. This even compression eliminates the imbalance common with sidelock holders, which push tools to the bore's edge, and reduces inertia for smoother, faster machining. Unlike fixed-diameter chucks, ER Collet Chucks offer flexibility through interchangeable collets, allowing a single chuck to support multiple tool sizes-simplifying inventory management and lowering operational costs.
Constructed from heat-treated spring steel, ER collets boast exceptional durability and resistance to wear, even under the stress of high-pressure coolant (up to 1100 psi for sealed models) and repetitive clamping cycles. Precision-ground surfaces ensure tight tolerances: standard ER collets typically achieve concentricity of 0.0004" TIR (Total Indicator Reading), with ultra-precision variants reaching 0.0002" TIR for critical aerospace or medical part manufacturing.
Features
The ER Collet Chuck's design is packed with features that address the most pressing needs of CNC machinists:
Ultra-Low Runout
By distributing clamping force evenly, the system minimizes runout (typically ≤0.0005"), which extends tool life by up to 30%-especially critical for carbide tools-and improves surface finish on machined parts.
Wide Clamping Range
Each collet size covers a flexible diameter range (e.g., ER16 handles 0.5–10mm, ER40 spans 2–26mm), reducing the number of collets needed in inventory. ER16 to ER40 models offer a collapse range of ~0.039", while smaller ER8/ER11 provide 0.5mm flexibility.
High Clamping Force
The 8° back taper (16° included) creates a mechanical lock, while the 30° front nose taper increases nut contact area for superior grip. Pairing with a bearing nut can double clamping force, and coated nuts further enhance performance.
Versatile Compatibility
Works with all round-shank tools (drills, end mills, taps, reamers) and integrates seamlessly with most CNC machines. Specialized variants include sealed collets (for 100% coolant delivery) and tap collets (with square drives for rigid tapping).
User-Friendly Design
Self-extracting collets eliminate the need for "collet squeezers"-simply unscrew the nut to release the collet, saving time during tool changes.
Durable Construction
Heat-treated steel resists corrosion and wear, while sealed collets use mechanical seals (superior to silicone) to block chips and dust, ideal for iron milling.
Applications
The ER Collet Chuck's versatility makes it indispensable across industries and machining tasks:
General CNC Milling
Handles roughing and finishing operations on metals (aluminum, steel, titanium) and plastics, delivering consistent accuracy for automotive components, brackets, and enclosures.
01
Precision Drilling & Reaming
Minimal runout ensures tight hole tolerances, making it ideal for aerospace parts (e.g., engine components) and medical devices (e.g., surgical instrument housings).
02
Rigid Tapping
Tap collets with square drives reduce clearance requirements and provide positive driving force, suitable for threading in high-volume production (e.g., electronics chassis).
03
High-Speed Machining
Low inertia and balanced design enable speeds up to 20,000 RPM+, critical for mold making and engraving where surface finish is paramount.
04
Multi-Material Processing
Effective for ferrous and non-ferrous metals, composites, and wood, with sealed collets preventing coolant contamination in wet machining.
05
Common end-users include automotive manufacturers, aerospace suppliers, job shops, and DIY enthusiasts-any operation prioritizing precision, efficiency, or cost savings.
FAQ
Hot Tags: er collet chunk for CNC, China er collet chunk for CNC manufacturers, suppliers, factory, Lathe Quick Center Block, ER Collet Chunk for CNC, machine accessories, Centre Drill Holder, Sleeve with Coolant, High Speed Boring Tool